

Why Are Temperature-Controlled Insulated Boxes Essential for Pharmaceutical and FMCG Products?
If you transport temperature-sensitive medicines or perishable food products, you already know that maintaining the correct temperature can make the difference between a safe product and a compromised one. A deviation of just a few degrees, even for a few hours, can affect the stability of a vaccine, reduce the effectiveness of a treatment or spoil refrigerated food intended for end consumers.
For companies in Romania operating in the pharmaceutical, FMCG, e-commerce or logistics sectors, maintaining the cold chain means responsibility, compliance and cost control. Temperature-controlled insulated boxes help you manage these requirements professionally, with minimal losses and clear traceability.
What Is Temperature-Controlled Insulated Packaging?
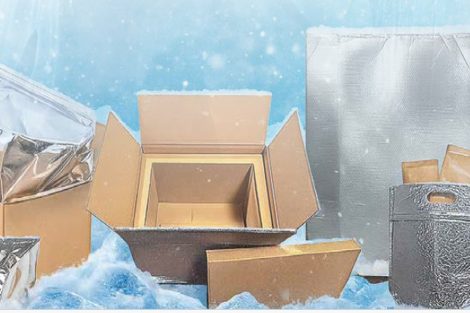
There are various types of insulated packaging with temperature control, designed to keep products within a clearly defined temperature range during transport or temporary storage. We are not talking about a simple insulated box, but about a system configured according to the product, delivery time and external conditions.
For example, for medicines that must be stored between 2-8°C, you should choose boxes tested for this range and equip them with correctly calibrated cold packs. For refrigerated food products, you can adapt the configuration according to the season and distance. On the dedicated page for temperature-controlled insulated boxes, you can find suitable options for pharmaceutical and FMCG applications, validated for professional use.
How Thermal Insulation Works
Thermal insulation reduces heat exchange between the interior and exterior. Materials such as EPS (expanded polystyrene) and other structures with controlled density slow heat transfer through conduction and convection.
A box with 40 mm walls will maintain a stable temperature for longer than one with 20 mm walls under the same external conditions. However, thickness is not the only criterion. Internal volume, the number of openings, the positioning of the cold packs and the product’s initial temperature also matter.
For stable results, always precondition products to the correct temperature before packing. Packaging maintains temperature; it does not actively cool the product if it is already dispatched above the permitted limit.
What a Complete System Includes
An effective cold-chain packaging system may include:
- a durable corrugated cardboard or plastic outer box;
- an EPS thermal insulation insert;
- cold packs or phase change materials;
- separators to prevent direct contact between the product and the cooling source;
- temperature loggers for monitoring.
The range of insulated packaging from INATECH Packaging covers these configurations and allows them to be adapted to the needs of each project.
Why Temperature Control Is Mandatory in the Pharmaceutical Industry
Most medicines have clear storage specifications: 2-8°C for vaccines and biological products, 15-25°C for many standard medicines, or below-zero temperatures for certain specialist therapies.
If the temperature exceeds the recommended limits, the active substance may degrade. In the case of insulin, for example, prolonged exposure to high temperatures reduces treatment effectiveness. Vaccines may become ineffective if the cold chain is interrupted.
This material is for informational purposes only and does not replace medical advice. Patients should always discuss the correct treatment storage conditions and any suspected exposure to unsuitable temperatures with their doctor or pharmacist.
What Risks Arise from Temperature Deviations?
For the patient, the risk means treatment with reduced effectiveness or unexpected reactions. For your company, the risks include:
- holding batches pending analysis;
- destroying compromised products;
- direct financial losses;
- non-conformities during GDP audits.
Good Distribution Practice regulations require transport conditions to be monitored and documented. Without suitable packaging and temperature recording systems, you cannot demonstrate compliance.
For standard use in pharmaceutical distribution, choose boxes validated for the actual transport duration and add a safety margin of at least 20-30% over the estimated time.
The Importance of Insulated Boxes in FMCG
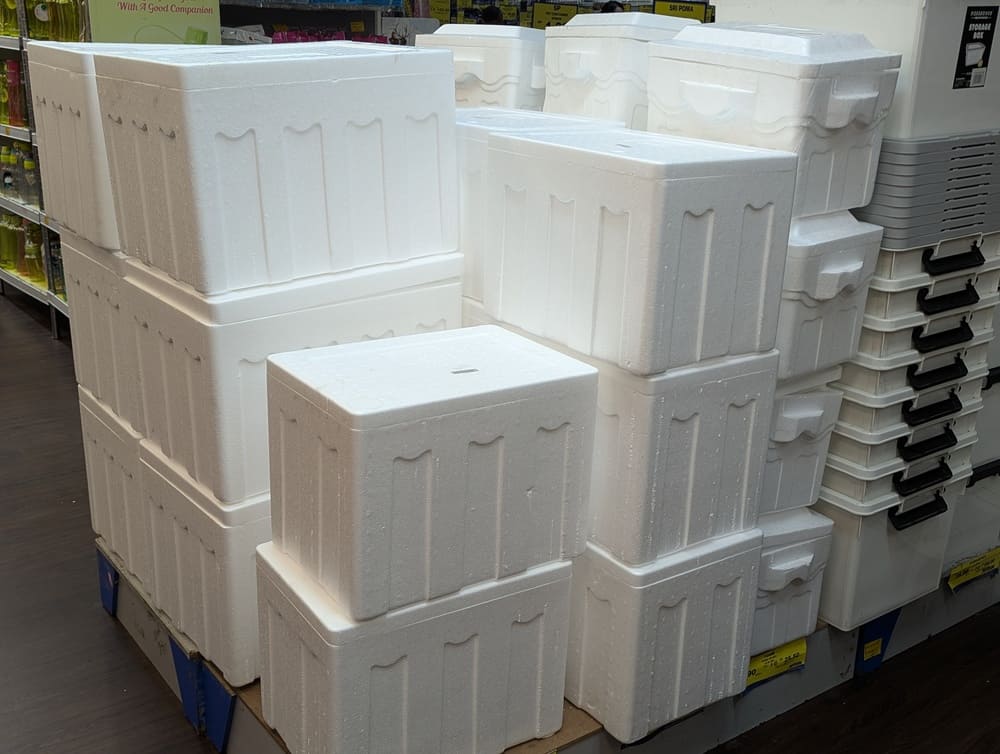
In FMCG, the pressure comes from volume and speed. Products move quickly, while margins are carefully calculated. Any damaged batch affects profitability and relationships with retailers or end customers.
Fresh meat, fish, dairy products, refrigerated desserts and heat-sensitive food supplements require controlled temperatures. An interruption of the cold chain encourages bacterial growth, which can lead to hygiene non-conformities.
For courier deliveries, especially in food e-commerce, you can use EPS thermal boxes configured according to the delivery duration and season. In summer, increase the number of cold packs and test the configuration under real conditions.
Food Safety and HACCP Standards
The HACCP system requires critical control points to be monitored, and temperature is one of them. If you deliver refrigerated products at 2-8°C and the temperature rises above the limit for too long, the product may become non-compliant.
Do not sell products suspected of having been exposed to unsuitable temperatures. Consult the food technologist or quality manager and apply your internal assessment procedures.
The right packaging helps reduce the risk of such situations and maintain the standards required by authorities and commercial partners.
How to Choose the Right Insulated Box
The choice should not be based on a single criterion. Analyse your specific application:
- What temperature must be maintained?
- How long will transport take?
- What is the estimated external temperature?
- What is the value of the goods being transported?
For urban transport lasting 2-3 hours, you can use a simpler configuration. For national distribution lasting 24-48 hours, you need thicker walls and careful sizing of the cold packs.
Also consider logistics costs. The box’s external volume affects the transport rate. Find out how to correctly calculate the impact on packaging and transport costs in the article about volumetric weight.
Common Mistakes
Many companies undersize the cooling system to reduce the cost per parcel. This may seem advantageous in the short term, but losses arise over the medium term.
Avoid these situations:
- using too few cold packs;
- failing to precondition cooling elements correctly;
- placing products directly next to the cold source and exposing them to freezing;
- failing to test the summer configuration when using the winter configuration.
For products that are also sensitive to humidity, you can integrate additional solutions. For example, in certain industrial applications, using desiccants helps control condensation inside the packaging.
Why Work with INATECH Packaging?
INATECH Packaging is a complete packaging solutions supplier with more than 14 years of experience in the Romanian market. The portfolio includes:
- insulated packaging for the pharmaceutical and FMCG sectors;
- e-commerce packaging;
- eco-friendly packaging and FSC-certified products;
- protective solutions for industries such as automotive, electronics, aerospace, construction and furniture manufacturing;
- packaging for sports and leisure.
In addition to products, you have access to professional packaging machinery and equipment, sealing systems, film-wrapping equipment and warehouse equipment. You can rent equipment, request technical support and benefit from dedicated consultancy to optimise your logistics flow.
Customisation and Availability
You can request custom dimensions for insulated boxes, internal configurations adapted to your products and branding applied to the packaging. The technical team analyses your requirements and proposes a solution that balances performance and costs.
The solutions are available for both industrial companies and non-industrial customers who need temperature-controlled transport, for example for events or special deliveries. Delivery is fast, and the products are designed for repeated use or recycling, depending on the type.
Frequently Asked Questions About Temperature-Controlled Insulated Boxes for Pharmaceutical and FMCG Products
What are temperature-controlled insulated boxes?
Insulated boxes are special packaging solutions designed to maintain a constant temperature, either cold or warm, during transport and protect products that are sensitive to temperature variations.
What types of products are they used for?
They are mainly used for pharmaceutical products such as vaccines, medicines and biological samples, as well as sensitive FMCG products including refrigerated and frozen food, dairy products, meat and ready-to-eat products.
What temperature ranges can they maintain?
The most common ranges are between 2°C and 8°C for the pharmaceutical cold chain, between 15°C and 25°C for controlled ambient temperature and below 0°C for frozen products.
How long can they maintain the temperature?
The duration depends on the box type, insulation material, cooling elements used and external temperature, but it can generally range from 24 to 120 hours.
What materials are used for insulation?
Commonly used materials include expanded polystyrene, expanded polypropylene, vacuum-insulated panels for high performance and polyurethane foam.
Do the boxes need to be validated?
Yes, especially in the pharmaceutical industry, where boxes must be validated in accordance with GDP standards to demonstrate that they maintain the required temperature throughout transport.
Can insulated boxes be reused?
Yes, many models are reusable, especially those made from durable materials such as expanded polypropylene, although single-use options are also available.
What role do cooling elements play?
Cooling elements help maintain the internal temperature and are selected according to the desired range and transport duration.
What is the difference between PCM and ice packs?
PCM materials maintain a constant temperature at their phase-change point, while ice packs (gel packs) are more affordable but offer less precise temperature control.
Do these boxes comply with regulations?
Pharmaceutical products must comply with GDP standards and other relevant international regulations, while FMCG products must comply with food safety requirements.
How do you choose the right box?
The choice depends on the product type, required temperature range, transport duration, external conditions and applicable regulatory requirements.
Can they be used for international transport?
Yes, these boxes are designed for use in road, air or sea transport, including over long distances and in varied environmental conditions.
To ensure the safety of pharmaceutical and FMCG products throughout the logistics chain, choosing high-quality temperature-controlled insulated boxes is essential. The right solutions help maintain product integrity, comply with regulations and optimise transport costs.
Choose the expertise and professional solutions offered by INATECH Packaging for efficient, validated insulated packaging. Contact the INATECH Packaging team for personalised advice and discover the best options for your logistics needs.