Cosul tau contine 0 produse
Cosul tau este gol.
 Thermal Boxes for Frozen Products (-15°C)
 Thermo Boxes for Refrigerated Products (+2°C ...+8°C)
 Thermo Boxes for Ambient Temperature Products (+15°C ...+25°C)
 Thermal Boxes for Transportation with Dry Ice
 Expanded Polystyrene (EPS) Boxes
 Thermo Fresh Boxes for Perishable Products
Thermal Boxes for Transportation with Dry Ice

Thermal Boxes for Frozen Products (-15°C)

Thermo Boxes for Refrigerated Products (+2°C ...+8°C)

Thermo Boxes for Ambient Temperature Products (+15°C ...+25°C)

Expanded Polystyrene (EPS) Boxes

Expanded Polystyrene (EPS) Boxes

Expanded Polystyrene (EPS) Boxes

Expanded Polystyrene (EPS) Boxes

Expanded Polystyrene (EPS) Boxes

Thermo Fresh Boxes for Perishable Products

Thermo Fresh Boxes for Perishable Products

Thermo Fresh Boxes for Perishable Products

Thermal Boxes for Frozen Products (-15°C)

Thermal Boxes for Frozen Products (-15°C)

Thermal Boxes for Frozen Products (-15°C)

Expanded Polystyrene (EPS) Boxes

Expanded Polystyrene (EPS) Boxes

Expanded Polystyrene (EPS) Boxes

Expanded Polystyrene (EPS) Boxes
Thermo Fresh Boxes for Perishable Products

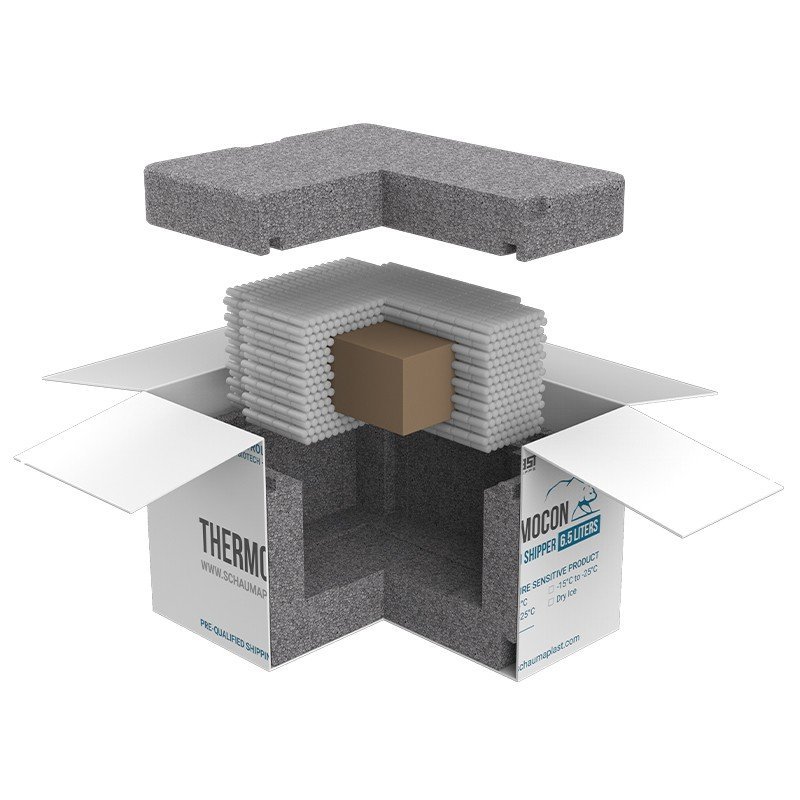
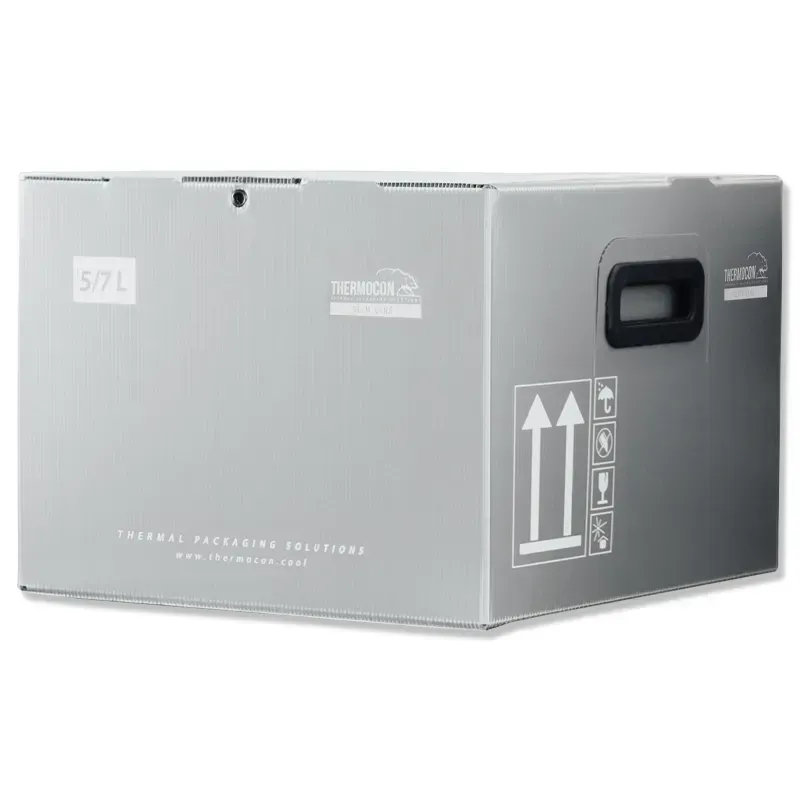
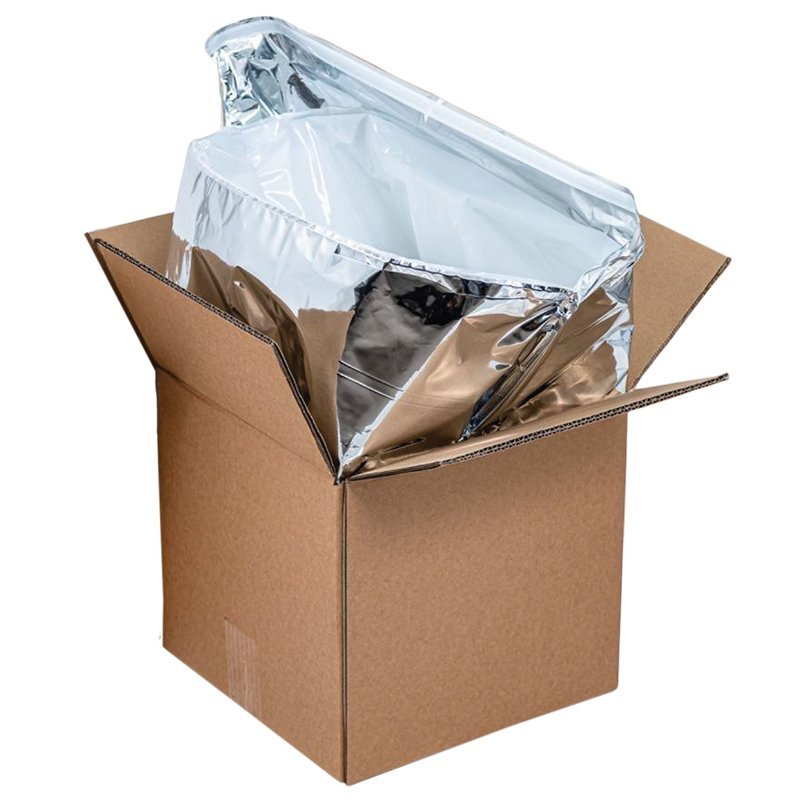
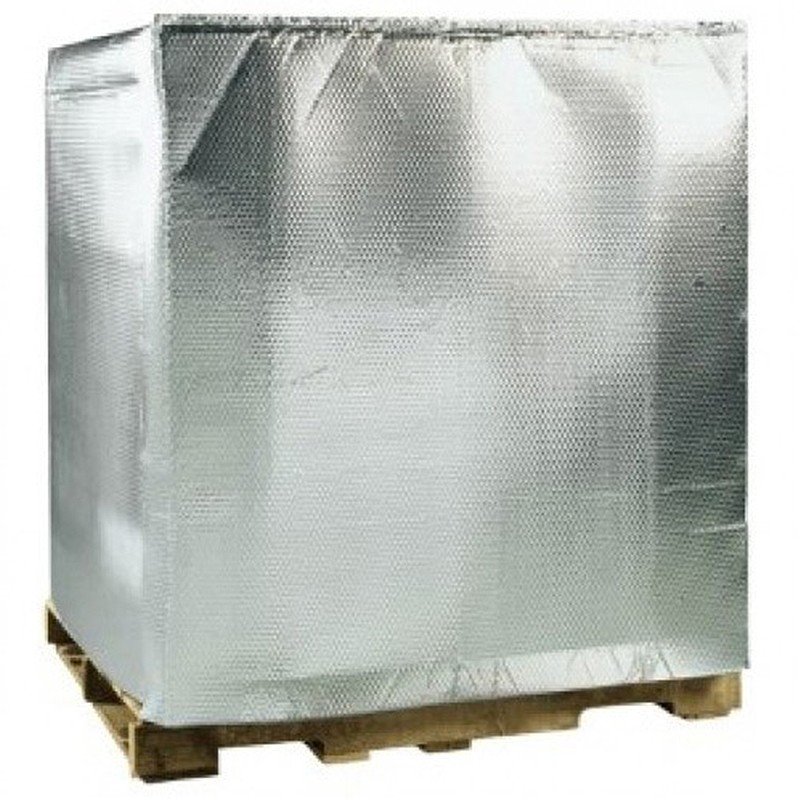
Temperature-controlled thermo-insulating boxes are technical packaging designed to maintain a stable temperature during the transport and storage of sensitive products. These boxes function as a thermal protection system, maintaining the necessary conditions so that the products do not lose their physical or chemical properties.
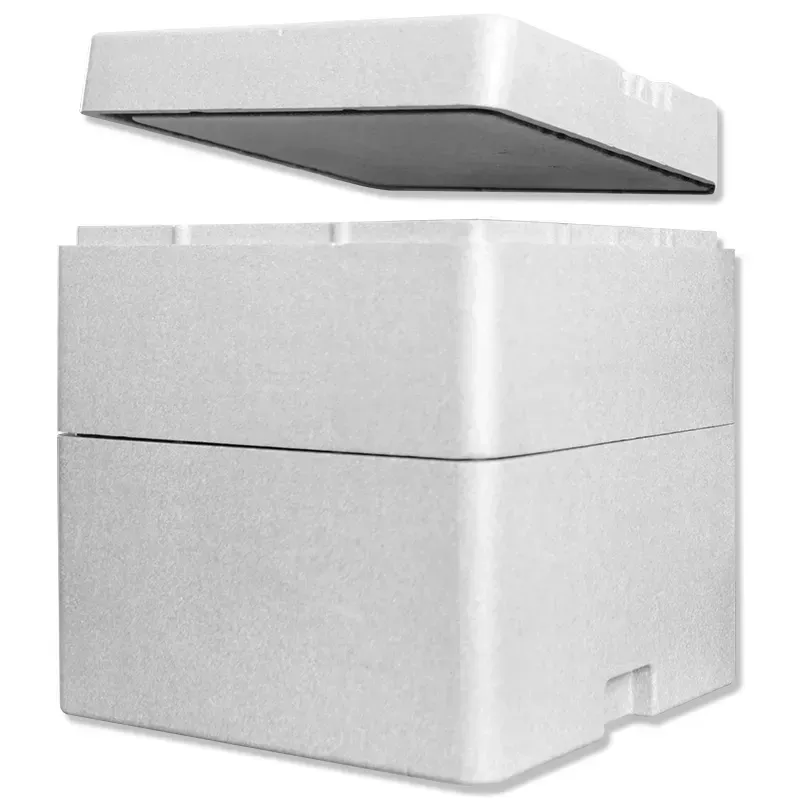
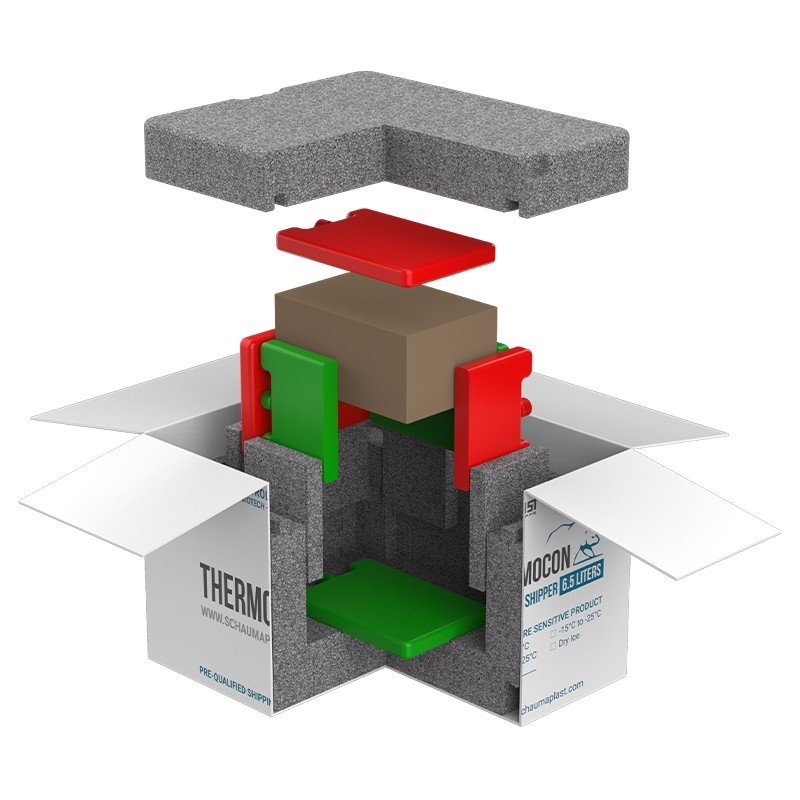
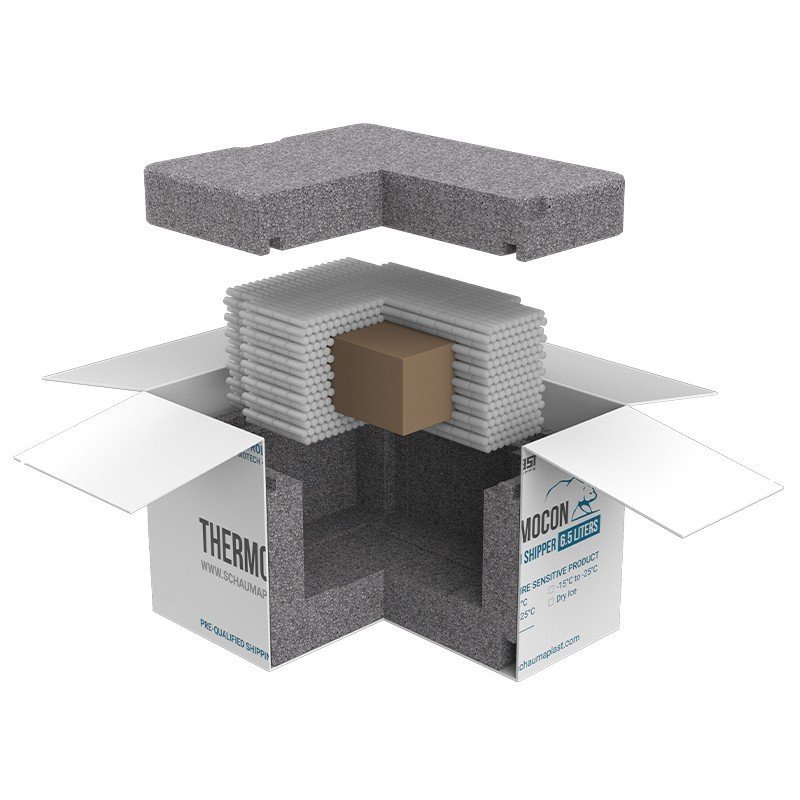
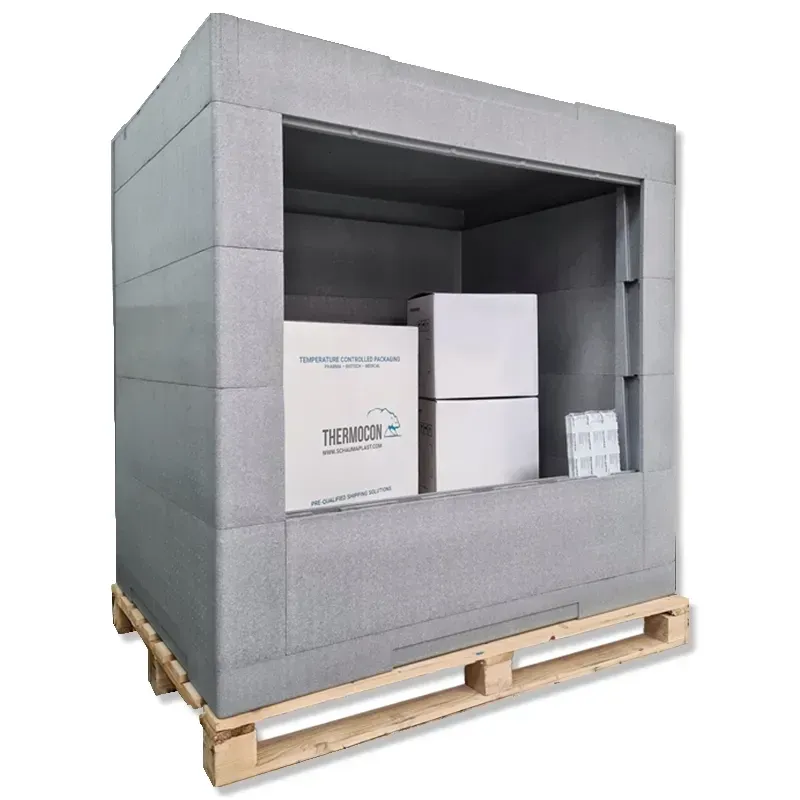
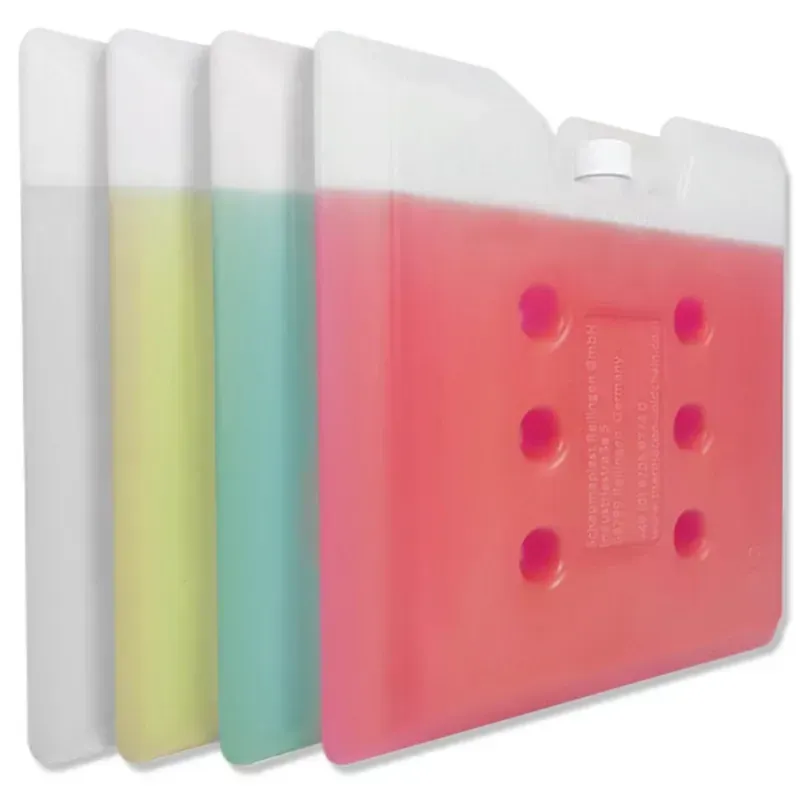
They are made from high-performance insulating materials, such as expanded polystyrene (EPS) or expanded polypropylene (EPP), which provides an efficient thermal barrier against heat transfer. Some models may include eutectic packs (ice packs), cooling plates or dry ice, meant to stabilize the temperature for periods of up to 120 hours. Thermo-insulating boxes are essential in logistic chains that require strict temperature control, such as the pharmaceutical, food or biological sample transport industries.
The use of these insulating packaging brings multiple logistical and economic advantages. First of all, they protect the products from temperature fluctuations, maintaining optimal storage parameters. This prevents the alteration or degradation of sensitive products.
Moreover, the boxes are lightweight, durable and reusable, designed for repeated use without loss of insulating capacity. The materials used are non-toxic and recyclable, contributing to reducing environmental impact.
Another major advantage is operational efficiency. Thanks to the ergonomic design and tight closure, the boxes can be easily handled, are compatible with standard pallets, and can be customized according to the product size or transport duration.
Temperature-controlled thermo-insulating boxes are indispensable in areas such as:
Depending on the need, the boxes are available for several temperature ranges:
These ranges can be maintained constant for tens of hours, depending on the box configuration and external conditions.
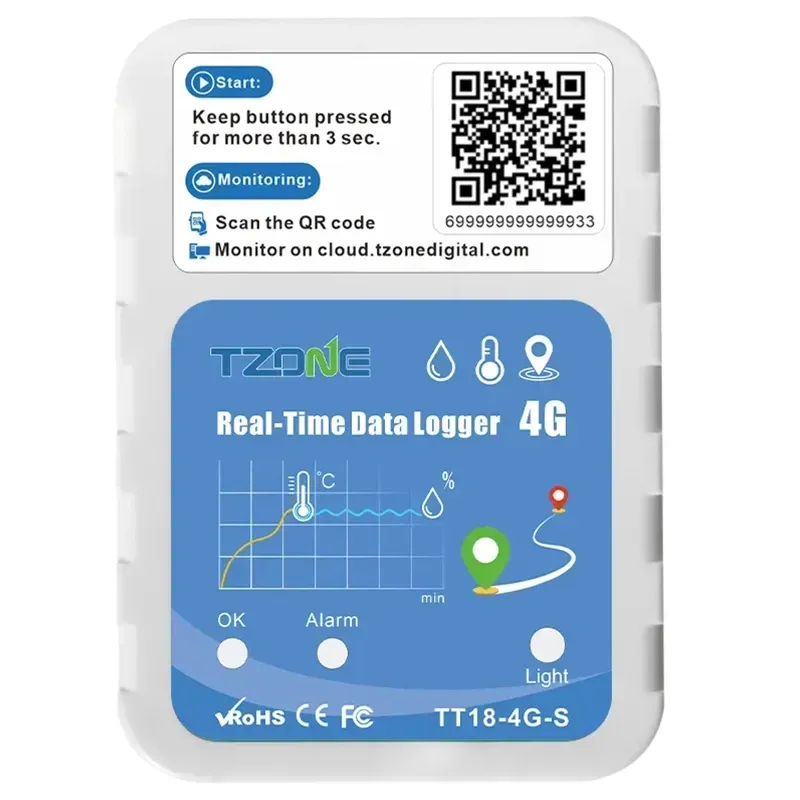
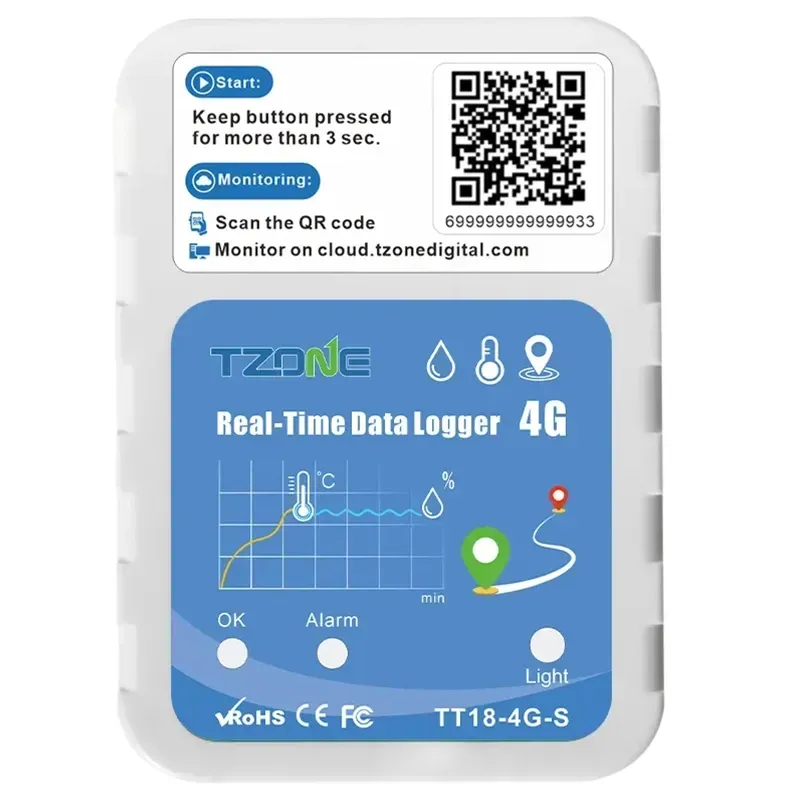
Thermo-insulating boxes can be completed with temperature monitoring systems, smart labels and digital sensors, offering complete traceability in the transport chain. In addition, certain models include caps with quick closure, tight seals and inserts for product separation.
The choice of the right box depends on the nature of the product, the duration of transport and handling conditions. A modern thermal packaging solution not only protects the content but optimizes costs and increases safety in the logistics chain.
The temperature-controlled thermo-insulating boxes from INATECH Packaging are an essential investment for any company that transports sensitive products. They guarantee safety, stability and compliance with standards in industries such as pharmaceutical and food.
By combining high-performance insulating materials with modern thermal control technologies, these boxes ensure efficient and constant protection, maintaining the quality of the product from the point of departure to the destination.
 Ecological Packaging
 Cardboard, Wood and Paper Packaging
 HoReCa Packaging
 Temperature Controlled Insulated Packaging
 VCI Packaging, ESD, Desiccants and Emitters
 Household Items and Labor Protection
 Adhesive Tapes and Glues
 Stationery and Office Supplies
 Warehouse Equipment and Consumables
 Bubble Wrap Packaging
 Stretch Film, Binding and Palletizing
 Professional Architectural and Auto Foils
 Machines and Consumables for Packaging
 Materials Used in Construction, Home and Garden
 Courier Envelopes and Bags
 Polyethylene, Polypropylene and Polyurethane
 Plastic Bags And Containers
Please sign in first.
Sign inCreate a free account to use wishlists.
Sign in